In aerospace electronics, margins for error are razor-thin. For engineering, quality, procurement, and operations leaders at original equipment manufacturers (OEMs), designing high-reliability hardware involves managing extreme thermal swings, intense mechanical vibration, and stringent functional requirements. A board that operates flawlessly in a CAD simulation can rapidly degrade on the factory floor if design constraints ignore manufacturing realities. How do decision-makers bridge theoretical electronic design with repeatable, flight-grade physical hardware?
The answer lies in structured Design for Manufacturability (DFM). Rather than treating DFM as a perfunctory rule-check at the end of layout, mission-critical programs require a comprehensive engineering assessment across three interconnected layers: board design, assembly process, and inspection or test strategy. While no design methodology eliminates every conceivable defect, this layered approach balances critical tradeoffs to significantly reduce scrap, rework, and program exposure.
Layer 1: The Board Design Foundation
The bare printed circuit board establishes the physical and thermodynamic boundaries of the entire assembly. Flaws introduced at this stage cannot be rectified during assembly without severe schedule and cost penalties.
Material Selection vs. Mechanical and Thermal Stability
Aerospace operating environments routinely subject assemblies to thermal cycling and high temperatures. Selecting high-Tg (glass transition temperature) laminate systems and materials with low coefficients of thermal expansion (CTE), such as specialized polyimides or high-performance FR-4 blends, is critical. However, high-reliability materials present distinct processing tradeoffs. Materials engineered for superior thermal resistance are often more brittle, requiring tighter parameters during mechanical drilling and routing to prevent internal delamination or micro-cracking.
Component Density vs. Thermal Dissipation
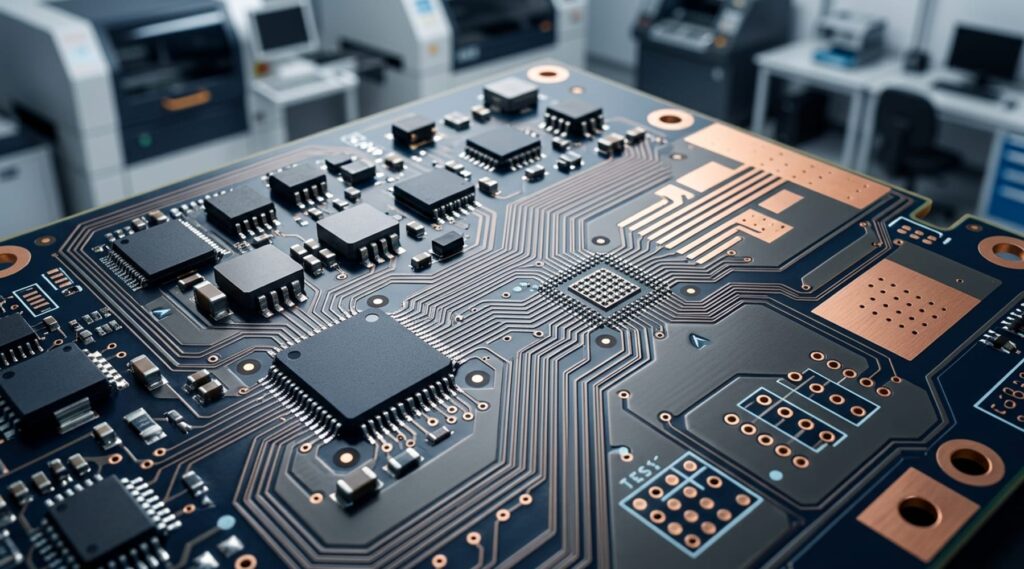
SWaP (Size, Weight, and Power) demands push aerospace designs toward higher component packaging densities. Cramming high-power processors, gate drivers, and passive components into tight board envelopes creates intense localized thermal hotspots. Mitigating this heat requires integrated thermal relief structures, such as solid copper planes, thick ground pours, and arrays of thermal vias.
Herein lies the classic layout tradeoff: while broad thermal copper balances operational temperatures in flight, it acts as a massive heat sink during manufacturing. Without precise thermal relief design on component pads, excessive copper draws heat away during soldering, resulting in cold solder joints, inadequate wetting, and uneven reflow across adjacent terminations.
Layer 2: The Assembly Process
Once bare board parameters are set, DFM must address the physical assembly environment. Pick-and-place precision, paste dynamics, and reflow profiles dictate production yields and long-term joint integrity.
Solderability and Surface Finishes
Surface finish selection represents an ongoing balance between shelf life, coplanarity, and solder joint metallurgy. Electroless Nickel Immersion Gold (ENIG) offers flat pad topography ideal for fine-pitch ball grid arrays (BGAs), but fabricators must rigorously control phosphorous content in the nickel layer to prevent brittle joint fractures. For assemblies requiring direct wire bonding or extended storage, Electroless Nickel Electroless Palladium Immersion Gold (ENEPIG) provides robust protection against corrosion, though at higher material and operational cost.
Panelization and Tooling Clearances
Subsystem boards rarely travel down an automated SMT line individually; they are panelized to optimize pick-and-place efficiency. In aerospace manufacturing, panel routing requires deliberate mechanical planning:
- Depaneling Stress: V-scoring introduces shear stress that can fracture brittle ceramic capacitors or damage sensitive microcircuits placed near board edges. Tab-routing with breakaway perforated tabs isolates functional circuitry from depaneling strain.
- Edge Clearance: Active traces and surface-mount pads must maintain adequate clearance from edge rails and route paths to prevent copper exposure or mechanical shock during singulation.
- Tooling and Clamping Zones: Board edges must accommodate conveyor rails, selective solder fixtures, and support pins without impinging on low-profile connectors or overhanging components.
Layer 3: Inspection and Test Strategy
Aerospace standards require verifiable quality metrics. A circuit that cannot be fully inspected or tested creates substantial verification risks during downstream qualification.
Balancing Fine Pitch with Optical and X-ray Visibility
The proliferation of bottom-terminated components, including BGAs, Quad Flat No-leads (QFNs), and land grid arrays, obscures solder joints from standard Automated Optical Inspection (AOI). Quality plans must incorporate Automated X-ray Inspection (AXI) to verify solder fill, detect bridging, and quantify voiding percentages against rigorous quality objectives.
Component layout dictates X-ray viability. Placing two complex BGAs directly opposite each other on top and bottom board layers complicates standard 2D transmission X-ray imaging, as the solder ball shadows overlap. DFM guidelines advise staggering dense array packages or planning for oblique angle computed tomography (CT) inspection to preserve inspection fidelity.
In-Circuit Test (ICT) and Flying Probe Access
Comprehensive electrical verification relies on physical test access. Miniaturization often tempts layout designers to eliminate dedicated test pads, relying instead on functional connector testing. However, omitting test pads severely limits early fault isolation.
- Dedicated Test Points: Providing accessible test pads on a consistent grid allows bed-of-nails or flying probe testers to verify continuity, passive component values, and net integrity before functional powering.
- Proximity to Tall Components: Test points placed too close to tall electrolytic capacitors, transformers, or structural hardware become inaccessible to mechanical test probes, forcing risky manual verification methods.
Actionable DFM Considerations for Decision-Makers
To institutionalize these parameters across cross-functional programs, aerospace teams should implement structured design gates:
- Quantify Thermal Balance: Standardize thermal relief patterns on all ground connections to balance operational heat dissipation with manufacturing solderability.
- Establish Packaging Clearances: Maintain minimum clearance rules between dense SMT components and mechanical board edges to absorb depaneling stresses safely.
- Design for Inspectability: Avoid mirrored placement of bottom-terminated packages on double-sided boards to ensure unobstructed X-ray verification.
- Protect Test Budgets: Prioritize test point real estate during the initial layout phase rather than attempting to fit test pads into leftover board margins.
The Strategic Value of Early Collaboration
Balancing board density, mechanical robustness, thermal dynamics, and test coverage is not an exercise in isolated design theory. It requires deep alignment between product development teams and the manufacturing floor. While design software catches rudimentary rule violations, it cannot replicate the practical insights gained from physical production lines.
Partnering early in the development lifecycle with an experienced, U.S.-based electronic manufacturing services provider gives OEMs the technical transparency required to evaluate these critical tradeoffs. Collaborative DFM reviews identify process sensitivities while changes can still be made seamlessly in CAD, protecting your program schedule, reducing rework cycles, and ensuring your high-consequence electronics meet rigorous aerospace demands.