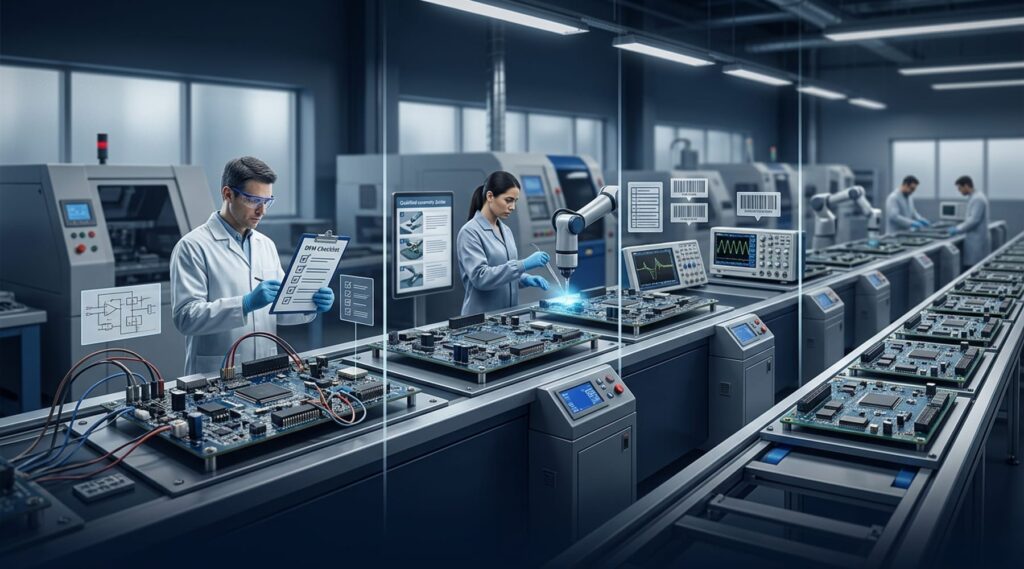
In defense electronics, moving from a functional benchtop proof-of-concept to repeatable, full-rate production is often the most vulnerable phase of a hardware program. A design that succeeds in lab testing can rapidly stall when confronted with high-mix surface mount line cadences, environmental screening parameters, and strict documentation mandates. Engineering, procurement, and quality leaders face a shared challenge: how do you establish a predictable, repeatable manufacturing baseline without sacrificing program velocity or absorbing unnecessary schedule and cost creep?
Bridging this gap requires disciplined gating rather than ad-hoc troubleshooting. The following six-stage roadmap provides a structured framework for taking complex defense assemblies out of prototyping and locking them into controlled, repeatable production.
Stage 1: Baseline the Design and Technical Data Package (TDP)
Objective: Establish a fully articulated, unambiguous definition of the hardware that reconciles schematic intent with physical fabrication realities before cutting production metal or ordering fabrication runs.
A functional prototype often relies on tribal knowledge between the design engineer and the technician. In production, ambiguity creates defects. The baseline Technical Data Package must contain fully resolved fabrication drawings, native CAD data, bills of materials (BOMs) with approved manufacturer part numbers (MPNs), assembly drawings with torque values, and clear workmanship callouts.
- Practical Evidence and Exit Criteria: Complete release of a rev-controlled TDP with zero unresolved drawing notes. Verification that every line item on the indented BOM matches active, procurable manufacturer part numbers. Confirmation of required IPC performance class parameters (such as IPC-A-610 Class 3 or J-STD-001 requirements where applicable) directly referenced on the master drawing.
- Key Risks to Watch: Discrepancies between Gerber or ODB++ fabrication layers and drawing dimensional callouts; unvetted alternate components inserted during prototype rework that never made it back to the official schematic; missing thermal relief or plane clearance specifications.
Stage 2: Close DFM and DFA Findings
Objective: Systematically identify and eliminate physical assembly bottlenecks, fabrication yield limiters, and reliability compromises before initiating pilot production.
Skipping or compressing Design for Manufacturability (DFM) and Design for Assembly (DFA) reviews does not save time; it simply pushes unresolved layout issues into high-cost production halts. Evaluating component spacing, copper distribution, thermal relief, and machine pick-and-place clearances ensures that high-density interconnects can be populated reliably at volume.
- Practical Evidence and Exit Criteria: Formally documented DFM/DFA report closed out with signed engineering dispositions for every flagged risk. Successful alignment on copper-to-edge clearances, aspect ratios, annular rings, solder mask web minimums, and probe access points for automated test equipment.
- Key Risks to Watch: Solder mask slivers between fine-pitch components that lift under reflow; via-in-pad applications lacking proper filling/capping specifications; inadequate component clear zones for automated optical inspection (AOI) or automated pick-and-place nozzles.
Stage 3: Qualify Manufacturing Processes
Objective: Prove that manufacturing methods, thermal profiles, tooling, and placement routines can repeatedly deliver compliant assemblies under production conditions.
Prototyping often involves manual placement adjustments or hand-soldering interventions that are unacceptable in high-reliability programs. Stage 3 transitions the build to automated lines, developing repeatable profiling for reflow ovens, selective soldering units, conformal coating systems, and mechanical torque tooling.
- Practical Evidence and Exit Criteria: Documented First Article Inspection (FAI) reports matching design dimensions and solder criteria. Thermal profiling logs verifying peak temperatures, ramp rates, and time-above-liquidus across the heaviest and lightest thermal mass components on the board. Validated automated optical inspection (AOI) and X-ray inspection recipes with confirmed coverage.
- Key Risks to Watch: Thermal shadowing on multi-layer high-copper boards leading to cold solder joints or incomplete barrel fill on through-hole pins; excessive thermal cycling during rework; uncalibrated production tooling causing mechanical stress on ceramic capacitors.
Stage 4: Lock Material and Production Traceability
Objective: Establish complete pedigree control over incoming components, raw materials, manufacturing routing, and assembly records.
Traceability in defense electronics protects the supply chain against non-conforming materials and unauthorized part substitutions. This stage ensures that every electronic component, PCB laminate lot, solder paste batch, and conformal coating container is systematically tracked to its specific subassembly serial number.
- Practical Evidence and Exit Criteria: Fully deployed serialization architecture capturing component lot codes, Certificates of Conformance (CoCs), and distributor tracking data. Approved moisture-sensitive device (MSD) handling logs and documented material travel records (travelers/routers) detailing operational sign-offs at each manufacturing step.
- Key Risks to Watch: Gray-market or unauthorized broker sourcing introduced to cover component lead-time gaps without OEM consent; incomplete sub-tier supplier documentation; co-mingling of different component date codes within a single assembly run without serial record updates.
Stage 5: Validate Test Coverage
Objective: Confirm that the selected suite of electrical, functional, and structural screening catches all critical manufacturing defects without introducing unintended stress.
Testing during prototyping typically centers on benchtop functional validation. Production test regimens, however, must rapidly verify structural integrity, component values, and basic continuity before subjecting the assembly to advanced operational screening. Bridging in-circuit test (ICT), flying probe, automated optical inspection, and final functional acceptance test (FAT) ensures high fault coverage across both visible and concealed joints.
- Practical Evidence and Exit Criteria: Quantified fault-coverage analysis showing verified coverage percentages for shorts, opens, component presence/orientation, and values. Repeatable automated test execution with stable gauge repeatability and reproducibility (GR&R) metrics, and documented environmental stress screening (ESS) procedures if mandated by the program.
- Key Risks to Watch: Relying exclusively on end-of-line functional pass/fail testing, which obscures intermittent contact or marginal solder integrity; test fixtures causing excessive board deflection during probe contact; lack of test points on dense layouts driving low fault visibility.
Stage 6: Manage Revisions Through Formal Change Control
Objective: Maintain absolute configuration control over designs, processes, and documentation throughout ongoing production cycles.
A hardware design is rarely static. Component obsolescence, performance enhancements, and manufacturing adjustments require continuous maintenance. Without strict Engineering Change Order (ECO) and Configuration Management (CM) procedures, unauthorized tweaks can quickly cause field failures or invalidate prior qualification testing.
- Practical Evidence and Exit Criteria: Established, auditable ECO processes detailing change justification, impact assessments on form-fit-function, customer review checkpoints, and controlled revision rollouts for work instructions and CAD assets. Documented scrap/rework dispositions for legacy revision hardware.
- Key Risks to Watch: Uncontrolled minor layout tweaks applied at the fab level without rev increments; silent part substitutions by component manufacturers; manufacturing lines operating against superseded work instructions.
Achieving Predictable Production Scalability
Transitioning defense electronics hardware from a functioning prototype to scalable, repeatable manufacturing is not a matter of luck. It relies on a rigorous, proof-oriented process that aligns mechanical, electrical, and process engineering across every phase of production. By baselining the TDP, closing DFM gaps early, qualifying production lines, enforcing traceability, validating test coverage, and controlling change management, defense OEMs can systematically reduce schedule, operational, and performance risks.
American Precision Electronics works with OEM engineering and quality teams to evaluate build readiness and navigate the transition to full-rate production. Contact our engineering team today to review your Technical Data Package and discuss a production-readiness review for your upcoming electronics build.